
 Tiếng Việt


When a customer brings a 3D file to the shop, the first question is usually “what wood is cheapest to mill this in?” The better question is “what is this pattern for, where will it sit, and will you take a mold from it afterward?” The same shape milled in pine, MDF or tooling board gives three very different results in accuracy, smoothness and lifespan. Pick the wrong material at the start and the sanding and priming afterward take twice the labor, sometimes the whole thing has to be redone.
This post doesn’t go back over how many axes a CNC machine has or how milling, carving and turning differ. You can read about that in the post on CNC woodworking with milling, carving, cutting and turning machines. Here we focus on one thing: choosing the material for a master pattern (also called a plug), then milling and finishing it to a standard good enough to take a mold from.
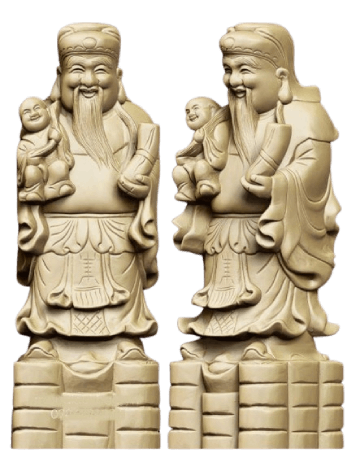
What is a master pattern and why does the material matter so much?
The master pattern is the “original” of the product. From it, you take a silicone mold, composite mold or plaster mold, or use it as a pattern for metal sand casting. Every defect on the master, even a small scratch or a raised wood grain line, is copied exactly to the mold, and from the mold to hundreds of products after it.
So the pattern material has to meet three needs at once. First, it must hold its dimensions, meaning that if you mill it today it is still the right size a week later. Second, the surface must come up smooth after sanding and painting. Third, it must survive what happens during moldmaking: release wax, solvents, the force of pulling the mold and the heat given off as resin cures.
If the pattern is only for a one-time display, the requirements are much lower. But if it is used to take a production mold, the cheapest material isn’t necessarily the one that saves money.
Natural wood: familiar, easy to find, but “alive”
Natural wood is the oldest pattern material. In metal casting, Western patternmakers have long favored sugar pine because it is light, soft and easy to work, with mahogany as the more durable choice. In Vietnam, shops often use imported pine, dipterocarp (gỗ dầu), oak or finger-jointed rubberwood, depending on what is available properly kiln-dried.
The biggest weakness of natural wood is that it always “breathes” with the humidity. Wood absorbs and releases water until it reaches equilibrium moisture content with its surroundings. When the wood’s moisture falls below the fiber saturation point, about 25 to 30% for most species, it starts to shrink noticeably. According to references on wood drying, shrinkage tangential to the growth rings is about 5 to 10%, radial about 2 to 6%, and along the grain only 0.1 to 0.3%. This uneven shrinkage in different directions is exactly why wood bows, cups and twists.
In a hot, humid place like Saigon, humidity differs quite a lot between the rainy and dry seasons. A board milled perfectly in March can open up at the joints in August if the wood wasn’t dried to suit its environment. Shop experience says always buy kiln-dried wood, let it “rest” in the shop for a few days before gluing up the stock, and glue up the stock from many strips with alternating grain so the shrinkage forces cancel each other out.
Natural wood still has its place. It is hard, takes impact well, holds screws firmly and is easy to repair (just build up or glue on a piece). For patterns that take repeated loads, such as sand casting patterns and support frames, or products where the customer wants to keep the wood grain, natural wood is still a sensible choice.
The downside when milling is the grain. Cutting against the grain tends to fuzz and tear out, especially on thin edges and curved faces. Wood has alternating hard and soft growth rings, so after sanding and priming, over time the soft wood absorbs more paint and the grain shows through on the surface again. Patternmakers jokingly call it “ghost grain”, and it is a real headache when you need a mirror finish for molding.
MDF: cheap, flat, easy to mill, but hates water
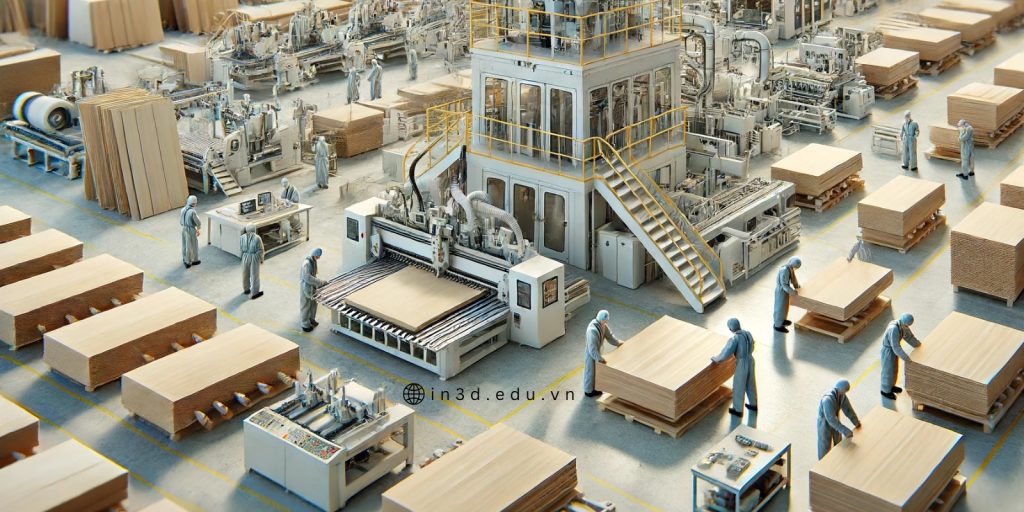
MDF (medium-density fibreboard) is board pressed from wood fibers mixed with resin. According to commonly cited figures, MDF is about 82% wood fiber, 9% urea-formaldehyde resin, 8% water and 1% paraffin wax, with a density usually between 600 and 800 kg/m³. Since it has no grain and no knots, MDF mills evenly in every direction. That’s why it is so popular for patterns, jigs, site models and architectural models.
When milling patterns in MDF, you’ll notice a few things. Flat faces come out very nicely and need little sanding. But curved faces that cut diagonally through the core of the board expose fibers that are more porous than the surface and soak up paint heavily. For patterns with many curved faces, you need several coats of primer or a thin coat of epoxy to “lock” the fibers before fine sanding.
MDF dulls cutters faster than natural wood because of the resin in the board, so shops usually use carbide cutters. MDF dust is very fine and plentiful. The urea-formaldehyde resin in the board can release formaldehyde, which IARC classifies as carcinogenic to humans, so milling MDF requires dust extraction and a good mask. This isn’t just talk; anyone who has stood next to an MDF milling machine all day will understand.
MDF’s fatal weakness is water. MDF generally has poor moisture resistance, and low-quality boards swell and crumble as soon as they absorb water, with the edges puffing up. An MDF pattern that isn’t fully sealed on every face with paint or resin will warp and swell in a humid environment. Moisture-resistant MDF (usually with a green core) is better, but still no match for tooling board.
Laminating several layers of MDF to get thick stock is common. Note that the glue lines between layers are harder than the surrounding MDF and tend to leave ridges when sanded. Use a thin glue layer, press evenly and avoid running glue lines through the most important surface areas of the pattern.

Tooling board: more expensive, but makes “production grade” patterns
Tooling board (or modeling board, often called PU board, epoxy board or artificial wood in Vietnam) is a synthetic resin board, mainly filled polyurethane or epoxy, made specifically for the patternmaking and moldmaking industry. Many major manufacturers around the world have product lines of this kind, grouped by density from low to high.
The biggest difference from wood is that tooling board has almost no grain and is very little affected by humidity. Mill it and leave it in a hot, humid shop, and it still holds its dimensions well. The milled surface is smooth and uniform, with no ghost grain. For patterns that need to produce a glossy mold, this is the advantage most worth paying for.
Density decides the use. Low-density boards are light and mill very fast, good for design models, ergonomic test models and display models. Medium-density boards suit master patterns for silicone and composite molds. High-density boards and epoxy boards have better hardness and thermal stability, and are used for casting patterns, vacuum forming molds, checking fixtures or working molds for small quantities.
Specific figures like density, heat resistance and thermal expansion coefficient vary by manufacturer, so check the data sheet for the exact board you buy. A general rule is that standard PU board has lower heat resistance than epoxy board, so when the mold sees high heat, lean toward epoxy.
The downside of tooling board is price. By volume, it costs many times more than MDF. Tooling board dust is also fine and needs good extraction. Some low-density grades are rather brittle at thin edges and chip easily on impact.

Heat when making composite molds
Many people pick a pattern material and forget the next step: taking the mold. When making a composite FRP mold, the worker brushes on gelcoat, then lays up fiberglass and resin over the master. Curing resin gives off heat (exotherm), and the thicker the layup, the higher the heat. Resin also shrinks as it cures, polyester about 5 to 6% and epoxy about 2%, and this shrinkage puts stress on the pattern surface.
With natural wood patterns, the heat dries the wood locally, which can cause hairline cracks in the paint or make the grain show. With MDF patterns, if the protective paint cracks, moisture and the styrene in polyester resin can seep in, blistering the surface and making the mold stick. With tooling board the risk is much lower, but you should still lay up in thin layers, wait for each to cool before the next, and never lay up too thick in one go.
Another issue is the release agent. Wood and MDF patterns must have their pores fully sealed with sealer or PU paint before several coats of release wax are applied. If the surface still absorbs, the wax sinks into the pores, the mold sticks and comes off pulling the paint with it. Anyone who has done composites for years has lost a pattern by skipping this step.
For a silicone mold, heat is negligible, but pay attention to the silicone type. Some platinum cure silicones are inhibited when they contact sulfur, some paints, adhesives or clays. Test the pattern on a small area before pouring the whole mold.

The shop process for CNC milling a wood master pattern
Every shop has its own way, but below is the process most patternmakers follow.
Step 1: Prepare the file and add allowances
Before milling, the 3D file must be prepared for its purpose. If the pattern is for metal casting, add a shrinkage allowance. Shrinkage is usually 0.6% to 2.5% depending on the metal; aluminum, for example, shrinks about 1.3%. Add draft, usually 1 to 3 degrees on outside faces and more on inside faces. If the pattern will get a thick paint coat, subtract the paint thickness on faces that need to be accurate. Read more about this in the post on custom metal casting patterns, composite casting patterns and scaling.
Step 2: Glue up the stock
The stock is the raw block of material before milling. Natural wood is glued up from strips with alternating grain. MDF and tooling board are laminated in layers with a suitable adhesive (tooling board usually uses epoxy or the manufacturer’s own adhesive). The stock must be at least a few mm larger than the pattern on each side to give the cutter room. For large patterns, glue up a hollow stock (stepped to follow the shape) to save material, especially when using tooling board.
Step 3: Roughing
Large cutter, deep cuts, with the goal of removing most of the material and leaving about 0.5 to 1 mm. With natural wood, let the stock rest a day or two after roughing. When a lot of material is removed, internal stress in the wood is released and the stock may bow slightly. Finish milling after the stock has settled is much more accurate.
Step 4: Finishing
Ball nose cutter, small stepdown. The smaller the stepdown, the finer the scallop marks, but the longer the machine run time. This is where you balance machine cost against sanding labor. With tooling board, you can finish mill very fine and it needs only light sanding. With natural wood, plan the toolpath to run with the grain as much as possible to reduce fuzzing.
Step 5: Seal and prime
Wood and MDF must be coated with sealer until they no longer absorb. Then fill defects with putty, apply a thick primer and sand from coarse to fine grit. You usually need to repeat a few rounds of priming and sanding. Tooling board has fewer pores, so the number of rounds drops significantly.
Step 6: Finish painting and polishing
Master patterns for composite molds are usually painted with 2K PU paint or coated with a pattern-specific tooling gelcoat, then wet sanded with fine paper and polished. However glossy the pattern surface is, that’s how glossy the mold will be. Finally, check dimensions with a ruler, gauges, or a 3D scan compared to the original file if requirements are high.
Quick comparison of the three materials in real situations
Instead of a dry scoring table, here are a few common situations.
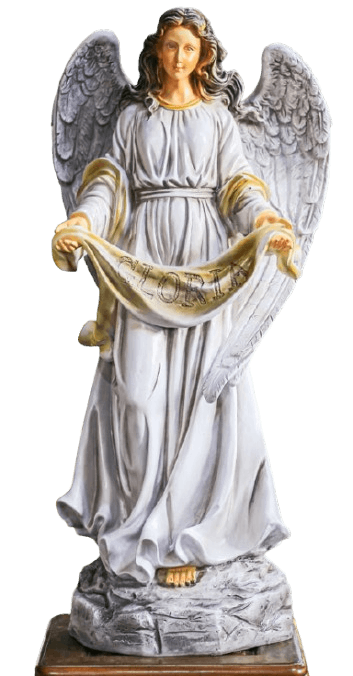
A 1 m decor statue pattern, molded in composite to make 50 pieces. The sensible choice is medium-density tooling board, or MDF if the budget is tight and you accept a lot of priming work. If the surface detail is very complex, people often rough mill in foam, apply a coating and then hand finish; see the post on CNC foam and CNC wood in rapid prototyping.
A sand casting pattern for an iron part, cast a few hundred times. Hard natural wood or high-density epoxy board. The pattern has to take rammed sand, impacts and being pulled out and put back many times. The post on CNC wood molds in this series goes deeper into sand casting.
A design model of an electronic product for customer approval, no mold taken. Low-density tooling board or MDF, milled quickly and painted nicely, is enough. If many small fitted parts are needed, 3D printing may be more economical.
A vacuum forming mold for plastic trays, a few hundred pulls. Epoxy board or heat-resistant tooling board, because hot plastic sheet is pressed onto the mold repeatedly. MDF can be used for a few dozen trial pulls, but will deteriorate quickly.
Large patterns several meters tall for stages or advertising. Wood and tooling board are both too heavy and too expensive; composite-coated foam is the right choice.

Cost: don’t just look at the board price
When pricing a master pattern, material is usually only part of the cost. Most of the rest is machine time, tooling, stock glue-up, priming, sanding, painting and the risk of redoing it. For example, MDF is cheaper than tooling board, but an MDF pattern with many curved faces may need several extra days of priming and sanding. Tooling board costs more, but after finish milling it can almost be painted right away, with little risk of warping.
Natural wood prices vary by species and drying quality. Cheap wood that isn’t dried properly will warp a few weeks after milling, and the cost of redoing it is the most expensive item of all.
To better understand what goes into pattern pricing, read the post on rapid prototyping and 3D printing costs. The most effective approach is still to send the 3D file so the shop can quote each material option, and compare total cost rather than board price.

Common mistakes when making patterns in wood and MDF
The first mistake is milling before the wood’s moisture has stabilized. The pattern looks great at delivery, but after some time in storage the joints open up.
The second mistake is not sealing MDF cut faces. The customer leaves the pattern in a damp warehouse, the edges swell a few mm and it loses its size.
The third mistake is priming thick to “fill” tool marks. Too much paint throws dimensions off, and a thick paint layer cracks easily under resin heat.
The fourth mistake is forgetting draft. The pattern is milled exactly to the product design file, but the design file has no draft, so the mold grips tightly and won’t release.
The fifth mistake is choosing low-density tooling board for a working mold. The board is soft, the surface scratches quickly and the mold deteriorates after a few uses.
Frequently asked questions
Can an MDF milled pattern be used to take a silicone mold?
Yes. The pattern just needs to be fully sealed with sealer and paint, the paint must be completely dry, and you should test how the silicone reacts on a small corner before pouring the whole mold.
Can tooling board be milled on an ordinary CNC wood router?
Yes, most tooling boards mill well on CNC wood routers with carbide cutters. You need good dust extraction because the dust is very fine.
How long does a wood pattern stay accurate?
It depends on the species, drying, glue-up and coating. Properly dried wood, glued up with alternating grain and fully sealed, can hold size for quite a while, but still falls short of tooling board in changing humidity.
When should I use 3D printing instead of milling wood?
When the pattern is small, has many negative features or deep pockets the cutter can’t reach, or needs many versions that keep changing. For large patterns with smooth curved surfaces, CNC milling is usually faster and cheaper.
Can several materials be combined in one pattern?
Yes, and shops do this all the time. For example, an MDF or foam core for the bulk, tooling board glued on important surfaces for finish milling, or added 3D printed details.
Need a master pattern in wood or tooling board?
CT3D offers CNC wood cutting and CNC foam cutting for master patterns, and can follow on with silicone molds or composite production in the same workflow. See the CNC machining services at CT3D Group and mold services. Send your 3D file or sample photos via Zalo/hotline 0975 008 728 for advice on the right material for the job.
References
- Wikipedia, “Medium-density fibreboard”: composition, density, moisture resistance and formaldehyde emissions of MDF. https://en.wikipedia.org/wiki/Medium-density_fibreboard
- Wikipedia, “Wood drying”: fiber saturation point, equilibrium moisture content and directional shrinkage of wood. https://en.wikipedia.org/wiki/Wood_drying
- Wikipedia, “Pattern (casting)”: casting pattern materials, shrinkage allowance and draft. https://en.wikipedia.org/wiki/Pattern_(casting)
- Wikipedia, “Fiberglass”: release agents and cure shrinkage of polyester and epoxy resins. https://en.wikipedia.org/wiki/Fiberglass

