
 Tiếng Việt


Customers often call us with a very familiar question: “I already have a master, now I want to cast 50 of them. What mold is cheap but durable?” If the part is large, the surface is fairly smooth and there aren’t many undercuts, the answer is usually a composite mold. People in the trade also call it an FRP (Fiber Reinforced Plastic) mold, a fiberglass mold, or in Vietnamese shop slang, a “phíp” mold.
This article is written the way a shop worker would explain it: what layers a composite mold has, the order you build them in, which resin to pick, how many pulls you can get, and when you should switch to a silicone mold instead of forcing a rigid one.
What is a composite mold, and what layers does it have?
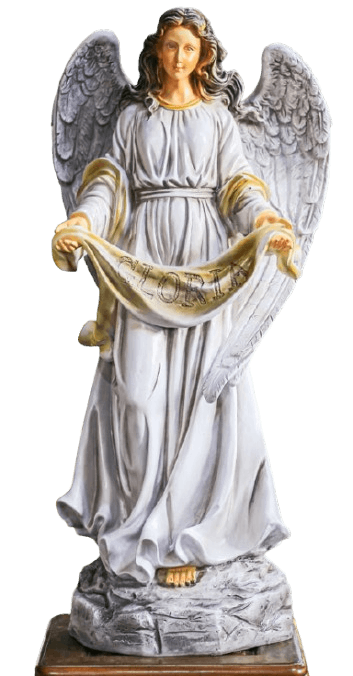
A composite mold is a rigid shell laid up directly on the master pattern (master, plug). Once it cures, the shell is separated from the pattern, and its inner cavity carries the exact shape and surface of the pattern. From then on, each casting is just a matter of applying material into the cavity and demolding the part.
A properly built FRP mold usually has three parts:
The first layer is tooling gelcoat. This is a thick, hard, wear-resistant resin layer that touches the part directly. According to Wikipedia’s article on gelcoat, this layer is usually about 0.5 to 0.8 mm thick, and the tooling grade has to withstand mechanical stress, curing heat and demolding forces. How good the part’s surface looks depends almost entirely on this layer.
The second layer is the resin-impregnated fiberglass laminate. The ply next to the gelcoat is usually a thin mat or a surface veil to keep the fiber pattern from printing through to the surface. Behind it are 300 or 450 g/m² mat plies alternating with woven roving for stiffness.
The third layer is the support frame. A small mold may only need extra thickness. A large mold must have ribs made of wood, steel tube or composite profiles so it doesn’t twist or bow when it’s laid down or when parts are pulled.
Multi-piece molds also have flanges along the parting line, drilled bolt holes and locating pins so the pieces fit back together tightly.
Why has composite been used for molds for so long?
Fiberglass isn’t a new material. According to Wikipedia, mass production of glass fiber was discovered in 1932, and the first composite boats appeared by the late 1930s. In 1953, the first Chevrolet Corvette launched with a glass-reinforced plastic body, with only about 300 built, almost by hand, in its first year. A GM body engineer later recalled that they first used plastic because they wanted to finish the show car quickly. That’s the same reason people in prototyping still like composite today: it’s fast, it doesn’t need big machines, and it’s easy to repair.
Britannica describes fiberglass as extremely fine glass fibers, widely used to reinforce plastics in boat hulls, car parts and wind turbine blades. It’s weather resistant, doesn’t rust and is light. For molds, we care about two more things: the mold is stiff enough to hold its shape, and light enough that two people can carry one piece of a mold for a two-meter statue.

Step 1: Prepare the master pattern carefully
A mold is only as good as its pattern. If the master has a 0.2 mm scratch, every one of the hundred parts after it will have that scratch too.
A master can be made in several ways. Small, detailed patterns are 3D printed in resin or hand-sculpted in oil-based clay. For large patterns like outdoor statues, mascots and 3D letters, we usually CNC-cut foam from the 3D file, apply a coat of filler and sand it smooth. If the customer only has a small model and needs it bigger, it gets 3D scanned and scaled up. The article on making casting patterns and scaling them to size covers this in detail. If you want to compare the cost of CNC versus 3D printing for a master, see the article on CNC foam and CNC wood in rapid prototyping.
There are three must-dos for the master before laying up the mold:
First, the surface must be sealed. Foam, wood and plaster all soak up resin. Without a sealer, the styrene in polyester resin will eat into EPS foam and the pattern will sink right while you’re laying up. New workers run into this a lot.
Second, draft angles. Any face parallel to the demolding direction should have at least 1 to 2 degrees of draft. An FRP mold is rigid and doesn’t flex like silicone, so even a small undercut will lock the part in. This is mostly a design issue, and the article on reverse engineering molds: tolerances, draft and shrinkage explains it clearly.
Third, plan the parting lines. Human and animal figures almost always need two, three or more pieces. We build dams from plastic sheet or clay along the parting line, lay up the first piece, then remove the dam and lay up the next piece against the flange of the previous one.
Step 2: Release with wax and PVA
This is the step many people rush, and it’s also the step that ruins the most patterns. Without enough release, the mold bonds permanently to the pattern. At that point the only option is to break the pattern to save the mold, or lose both.
The common approach is a silicone-free mold release wax. On a new pattern we usually apply 4 to 6 coats, letting each coat dry 15 to 20 minutes before buffing. After that you can spray a thin coat of PVA (polyvinyl alcohol) as a barrier film. PVA is water soluble, so it washes off easily after demolding.
A small but important note: don’t use car wax that contains silicone. Silicone on the surface makes gelcoat pull back into little craters called fish eyes, which are very hard to deal with later.

Step 3: Apply tooling gelcoat
Tooling gelcoat is usually catalyzed with MEKP at about 1.5 to 2% depending on temperature. In Ho Chi Minh City at 33°C, resin kicks much faster than during the cold season in the north, so you need to adjust the catalyst and mix small batches.
Gelcoat can be brushed or sprayed. We usually apply two coats, each about 0.3 to 0.4 mm thick, which adds up to the recommended 0.5 to 0.8 mm. Tooling gelcoat is usually black or orange, a different color from the part, so when you lay up parts it’s easy to see where coverage is even.
When you lay the first fiber ply matters a lot. Shop workers test it by lightly touching the edge of the gelcoat: if it’s tacky but doesn’t leave a fingerprint, it’s ready. Lay up too early and the styrene from the laminate wrinkles the gelcoat like alligator skin (alligatoring). Lay up too late and the two layers don’t bond well, and after a few pulls the gelcoat flakes off in patches.
Step 4: Lay up fiberglass and choose the resin
Polyester, vinyl ester or epoxy?
According to the literature on FRP, the three most common thermoset resins are polyester, vinyl ester and epoxy. Each has its place in moldmaking:
Polyester is the cheapest, easiest to buy and easiest to work with. The downside is high shrinkage and strong exotherm during cure. If you lay up too thick at once, the mold can warp and the fiber pattern can print through the gelcoat.
Vinyl ester costs more than polyester but shrinks less, is tougher and handles heat better. Many shops use vinyl ester for the first two plies behind the gelcoat (the skin coat), then polyester for the rest to balance cost.
Epoxy gives the most dimensionally stable mold with very low shrinkage, but it’s expensive and needs a matching gelcoat and wax system. Epoxy is usually reserved for technical part molds that need accuracy, or molds used to make epoxy or carbon fiber parts.
For molds for statues, decorative models and décor products, a vinyl ester plus polyester combination is what we use most.
Hand lay-up
Hand lay-up is the most common way to build a mold. Fiber plies are placed on the mold, wetted out with resin and rolled. According to Wikipedia, this method is used for canoes, kayaks and surfboards, and it can be combined with vacuum bagging for better consolidation.
The sequence we usually follow:
- The first ply is 225 or 300 g/m² mat, torn into small pieces and rolled carefully to push out all the air at sharp corners.
- Let this ply partially cure, and avoid laying up too thick at once, which causes heat buildup.
- The following plies alternate 450 mat and 600 or 800 g/m² woven roving, about 2 to 3 plies per session.
- Total mold thickness depends on size: a small mold under 50 cm is about 4 to 6 mm, and a mold over one meter is usually 8 mm or more, with a support frame.
Watch the resin-to-mat ratio too. Chopped strand mat takes a lot of resin, usually about 2 to 2.5 parts resin to 1 part fiber by weight. Too little resin leaves the fiber dry and white, and the mold is brittle. Too much resin makes the mold heavy, brittle and prone to shrinkage.
Air bubbles are enemy number one. Bubbles right behind the gelcoat will break open after a few pulls and leave pits in the mold surface. A grooved aluminum roller is a tool you can’t do without.
Spray-up
For large molds or parts, many shops use a chopper gun that sprays chopped fiber mixed with resin. It’s fast and cheap, but according to Wikipedia, strength and dimensional accuracy are lower than hand lay-up. We only use spray-up for the back layers of a mold, and the plies next to the surface are still laid by hand.
Step 5: Reinforce, cure and demold
Large molds must get their frame while the laminate is still on the pattern. If you attach the frame after demolding, the mold has already sagged under its own weight and is no longer true to shape.
After lay-up, leave the mold on the pattern for at least 24 to 48 hours. Shops that build molds carefully also post cure at around 40 to 60°C so the resin fully cures before demolding. A mold pulled too early is still “green,” and it can distort and keep shrinking over the next few days.
To demold, drive plastic or wooden wedges gradually into the flange edges. Don’t pry with a steel screwdriver, since it easily chips the gelcoat. Some molds have built-in ports for blowing compressed air between the mold and the pattern, which makes separation much gentler.

Step 6: Finish the mold surface before the first pull
A freshly demolded mold is rarely perfect. We usually wet sand it with 800 grit, then 1500 and 2000, then polish it with polishing compound. Small pinholes are filled with gelcoat.
Before the first pull, a new mold needs to be “broken in” with 4 to 6 coats of release wax, just like the master pattern. Skip this and the first part will almost certainly stick.
How many pulls can a composite mold give?
This is the question customers ask most, and the honest answer is: it depends on how the mold is made and how it’s cared for.
An FRP mold built to the proper process, with tooling gelcoat and a vinyl ester skin coat, and maintained regularly, can give anywhere from a few dozen to a few hundred pulls before it needs major repair. A rushed mold made with standard gelcoat and all polyester may start pitting after only 10 to 20 pulls.
Things that wear molds out fast:
- Demolding parts with metal tools, which chips the edges.
- Not re-waxing regularly. As a rule, apply a fresh coat every few pulls.
- Casting high-exotherm materials such as thick resin pours, which “cook” the tooling gelcoat and cause crazing.
- Leaving the mold in the sun, which warps it and fades the gelcoat.
For comparison, CT3D’s silicone mold service page notes that silicone molds for art pieces or PU casting typically last about 20 to 100 parts, and when you need high volume from one pattern, you should move to a composite or rigid mold. That matches general experience in the trade.
Composite mold or silicone mold: how to choose?
These two mold types don’t fully replace each other. Here’s how we usually break it down by real situations:
Choose a composite mold when the part is large, 60 cm or more, the surface is fairly smooth with few undercuts, and you need many pulls. Examples: planters, tanks, machine housings, park benches, large décor statues, architectural cladding panels and GFRC products.
Choose a silicone mold when the pattern has lots of fine detail, deep relief or undercuts, and needs a flexible mold you can peel off. Examples: small statues, deep-carved reliefs, souvenirs, PU cast parts, candles and soap. Silicone also comes in many types, and picking the wrong one can ruin the job. The article on platinum-cure vs. tin-cure silicone in this series covers it in detail.
Combine both when the part is large and highly detailed. The inner layer is a thin silicone skin that captures the detail, and the outside is a composite shell that holds the shape (mother mold, jacket). This is very common for religious statues and large portrait statues. You use less silicone, so the cost drops a lot compared with pouring a solid silicone block.
On cost, a silicone mold is mostly material, since silicone is expensive per kilo. A composite mold uses much cheaper material but takes more labor: lay-up, a more carefully finished master, and splitting into pieces. For small patterns cast a few dozen times, silicone is usually more economical. For large patterns cast many times, composite clearly wins. The article on rapid prototyping and 3D printing costs breaks down what drives the price, and it applies to pricing molds too.
Besides these two, for some parts that need high rigidity in moderate quantities, a CNC wood mold is also worth considering.

What can you cast in a composite mold?
FRP molds can cast quite a few materials:
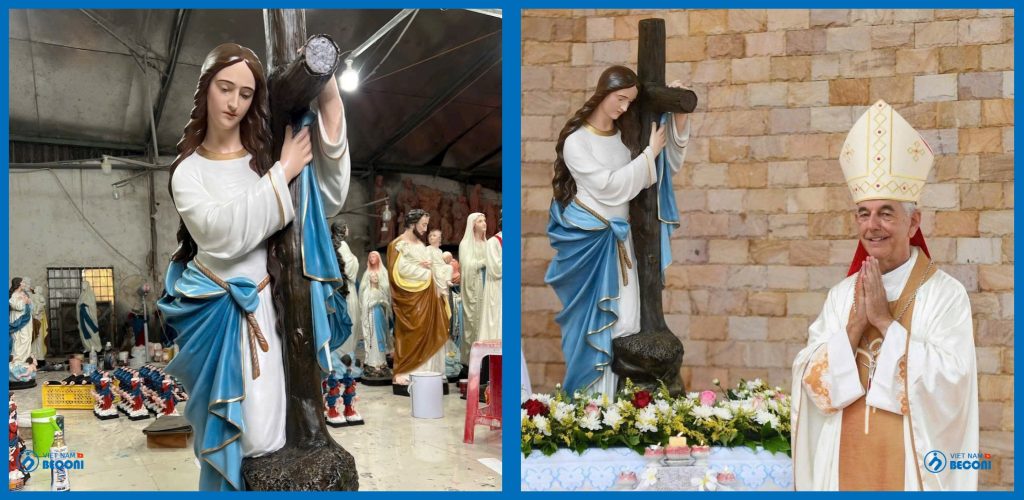
FRP composite is the most common use. The part is made with the same sequence: part gelcoat, fiber lay-up, cure, demold. According to CT3D’s composite statue production page, composite statues are about 30 to 50% lighter than stone or concrete, can last outdoors about 5 to 10 years or longer with a properly applied UV-protective paint, and production usually takes 3 to 10 days depending on size.
Glass fiber reinforced concrete (GFRC) and decorative cement. The mold needs more careful release because cement is alkaline.
Cultured stone, poly stone and solid resin casts for small and medium parts. Watch the heat released by thick pours.
Vacuum-formed and thermoformed plastic sheet for small runs, if the mold is made with heat-resistant epoxy.
If you’re interested in how shops increase output when casting composite statues in volume, see the article on improving quality and output in composite statue production.
Common mistakes when making composite molds
Collected from our own failures and from molds customers have brought in for repair:
Mold stuck to the pattern. The cause is almost always too few coats of wax, or a foam pattern that wasn’t fully sealed, so resin soaked in.
Wrinkled gelcoat. Fiber was laid up too early while the gelcoat was still wet, or the gelcoat was too thin.
Fiber pattern showing on the mold surface (print-through). There was no veil or thin mat right behind the gelcoat, or too many polyester plies were laid at once, causing heavy shrinkage.
Warped mold. It was pulled off the pattern too early, had no support frame, or was stored at the wrong angle.
Gaps at the flanges and thick flash at the seams. The flanges were laid up too thin, weren’t flat enough, or lacked locating pins.
Air bubbles in sharp corners. The inside corner was too sharp for the fiber to follow. Add a small radius to the corner on the pattern, or fill the corner with resin putty before laying fiber.
One more thing you can’t skip is safety. Britannica notes that exposure to fiberglass can cause eye irritation, sore throat, rashes and skin redness. The styrene in polyester has a very strong smell. Build molds in a ventilated area and wear an organic vapor respirator, nitrile gloves and long sleeves.
Real example: a mold for a set of 1.2 m planters
To make it concrete, here’s a fairly typical job. The customer needed 80 composite planters, 1.2 m tall, with vertical ribs on the outside.
The master was modeled in 3D, CNC-cut from EPS foam, then filled and primed. Because the planter tapers toward the top, a two-piece vertical split was enough, with draft already built into the design. The mold used black tooling gelcoat, a vinyl ester skin coat and polyester for the back plies, about 8 mm thick, with a square steel tube frame.
From file sign-off to a test casting took about two weeks, mostly spent on the master and waiting for the mold to cure. After that, each mold produced one to two parts per day. To go faster, you make two or three molds from the same master. If you poured a solid silicone mold for a pattern this size, the silicone alone would cost many times more than the FRP mold, and a large flexible mold would sag during casting.
Frequently asked questions
Can a composite mold handle parts with undercuts?
Yes, but you need extra mold pieces or loose pieces. The more undercuts, the more pieces, and at that point a silicone mold with a composite shell is usually the better choice.
How long does it take to make a composite mold?
A small mold can be done in 3 to 5 days if the master already exists. Large multi-piece molds usually take one to several weeks, depending on master work and cure time.
Do I need a physical master, or can the mold be made from a 3D file?
You need a physical pattern to lay up the mold on. If you only have a file, the master will be 3D printed or CNC cut from it.
Can a composite mold be used to cast clear resin?
Yes for thin parts, but thick resin pours release a lot of heat and can damage the tooling gelcoat. Small clear parts are usually cast in platinum-cure silicone molds for a better surface.
How should I store the mold?
Clean it after every pull, re-wax regularly, keep it in a dry, shaded place, and support it at the frame’s proper rest points.
Conclusion
Composite molds aren’t hard, but they demand discipline at every small step: the pattern must be sealed, the wax must be sufficient, the gelcoat must be timed right, the fiber must be rolled free of air, and you have to wait long enough. Done right, one mold can serve hundreds of parts.
If you have a pattern you need to replicate, or just an idea, the CT3D team handles everything from 3D scanning, design and master making to moldmaking and composite project construction. The CT3D Group mold services section has more information. Send photos or files via hotline/Zalo 0975 008 728 for advice on the right mold type.
References
- Wikipedia, “Fibre-reinforced plastic”: https://en.wikipedia.org/wiki/Fibre-reinforced_plastic
- Wikipedia, “Gelcoat”: https://en.wikipedia.org/wiki/Gelcoat
- Encyclopaedia Britannica, “Fiberglass”: https://www.britannica.com/technology/fiberglass
- Wikipedia, “Chevrolet Corvette (C1)”: https://en.wikipedia.org/wiki/Chevrolet_Corvette_(C1)
- CT3D, “Composite statue production”: https://in3d.edu.vn/san-xuat-va-thi-cong/san-xuat-tuong-composite/

